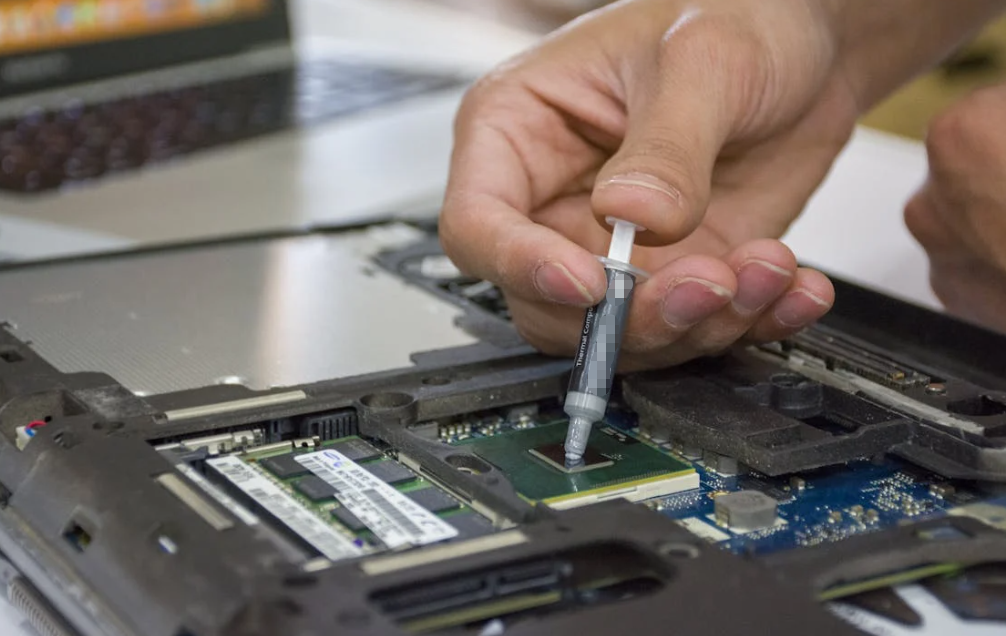
Mỡ tản nhiệt cho các mô-đun công suất lấp đầy những khoảng trống siêu nhỏ giữa tấm đế của mô-đun và bộ tản nhiệt hoặc tấm nguội làm mát bằng chất lỏng. Bằng cách thay thế không khí bị mắc kẹt bằng vật liệu dẫn nhiệt tốt hơn, mỡ giúp giảm điện trở nhiệt tiếp xúc và hỗ trợ nhiệt thoát khỏi IGBT, các mô-đun SiC MOSFET và các mô-đun công suất thông minh. Sản phẩm phù hợp không đơn giản là loại mỡ có giá trị W/mK cao nhất. Đó là loại mỡ tạo thành một lớp tiếp xúc mỏng, phủ kín và ổn định trong cụm lắp ráp thực tế.

Sự khác biệt này rất quan trọng. Một vật liệu tốt vẫn có thể hoạt động kém khi bộ tản nhiệt không phẳng, lớp vật liệu được phủ quá dày, trình tự siết vít làm cong tấm đế hoặc mỡ bị dịch chuyển trong quá trình chu kỳ nhiệt. Nói cách khác, mô-đun, mỡ, bề mặt làm mát, phần cứng lắp đặt và quy trình thi công hoạt động như một hệ thống thống nhất.
Hướng dẫn này giải thích cách lựa chọn hệ thống đó. Nội dung bao gồm các đặc tính vật liệu cần so sánh, kiểm soát độ dày đường keo thực tế, in stencil, các dạng hư hỏng thường gặp, các lựa chọn thay thế, tiêu chuẩn và thẩm định sản xuất. Luôn xem hướng dẫn lắp đặt của nhà sản xuất mô-đun là căn cứ cuối cùng đối với hình học và yêu cầu siết cố định của mô-đun.
What Does Thermal Grease Do in a Power Module Assembly?
Thermal grease does not cool a module by itself. It improves contact at the module-to-cooler interface. Even machined metal surfaces contain peaks, valleys and slight shape errors. When two dry surfaces are clamped together, those irregularities trap insulating air. Grease wets the surfaces and fills the small voids, creating a more continuous path for heat.
The heat path from the semiconductor junction to the coolant or air
Heat begins at the semiconductor junction. It then travels through the die attach, substrate, internal conductors and baseplate, where present. From there, it crosses the thermal interface material and enters a heat sink or cold plate. Finally, it moves into air or coolant.
The grease occupies only one thin part of that path, but it can become a bottleneck. Think of it like a gasket between two sections of pipe. The gasket is short, yet a poor fit can restrict the whole flow.
Engineers commonly track several resistance terms:
- Rth(j-c): junction-to-case thermal resistance inside the module.
- Rth(c-h): case-to-heat-sink resistance, strongly influenced by the interface.
- Rth(h-a) or cooler-to-fluid resistance: heat rejection from the cooling hardware.
- Rth(j-a): the complete junction-to-ambient path.
Grease selection mainly affects Rth(c-h), but a temperature problem should still be investigated across the whole stack. A better TIM cannot rescue an undersized cold plate or poor coolant flow.
Baseplate and baseplate-less modules need different thinking
A conventional IGBT module may have a metal baseplate that spreads heat and provides a mounting surface. Some newer SiC modules use thinner baseplates, exposed ceramic structures or baseplate-less designs to reduce thermal mass and internal resistance. These designs can be more sensitive to local pressure, flatness and insulation requirements.
Do not assume thermal grease provides electrical isolation. Many greases are electrically non-conductive, but the thin grease layer is not automatically a certified dielectric barrier. If isolation is part of the safety design, verify the module construction and use a qualified insulation solution.
Để có cái nhìn tổng quan hơn về mỡ tản nhiệt, miếng đệm, gel và các vật liệu khác vật liệu dẫn nhiệt giao diện, hãy bắt đầu bằng việc xác định khe hở thực tế và cấu trúc điện trước khi lựa chọn dạng vật liệu.
Bắt đầu từ bề mặt tiếp xúc, không phải con số độ dẫn nhiệt
Độ dẫn nhiệt mô tả mức độ dễ truyền nhiệt qua toàn bộ khối vật liệu. Đây là thông số hữu ích, nhưng không phản ánh độ tiếp xúc bề mặt, chiều dày cuối cùng hoặc sự lão hóa. Điện trở nhiệt giao diện ở cấp độ cụm lắp ráp là tổng của điện trở nhiệt trong khối vật liệu và điện trở tiếp xúc tại cả hai bề mặt. Mỡ có độ dẫn nhiệt ở mức vừa phải nhưng lan thành một lớp mỏng, liên tục có thể cho hiệu quả tốt hơn sản phẩm có độ dẫn nhiệt cao hơn tính theo W/mK nhưng vẫn dày hoặc để lại các khoảng rỗng.
Đối với một lớp đồng nhất được đơn giản hóa:
R = t / (k x A)
Ở đâu:
- R là điện trở nhiệt khối.
- t là độ dày đường keo.
- k là độ dẫn nhiệt.
- A là diện tích tiếp xúc hiệu dụng.
Công thức này hữu ích, nhưng các mối nối thực tế phát sinh thêm điện trở tiếp xúc. Độ nhám bề mặt, khả năng làm ướt, áp suất và hình dạng chất độn đều ảnh hưởng đến phần điện trở bổ sung này. Vì vậy, không nên chỉ sử dụng giá trị độ dẫn nhiệt trong bảng dữ liệu kỹ thuật để dự đoán nhiệt độ mối nối.
Sự phân biệt giữa độ dẫn nhiệt và tổng trở nhiệt đặc biệt hữu ích trong giai đoạn sàng lọc ban đầu.
| Datasheet term | Những gì nó nói với bạn | What it does not tell you | How to use it |
| Thermal conductivity, W/mK | Bulk heat-transfer potential | Final contact quality or bond line | Compare materials tested by a clear, comparable method |
| Thermal resistance, K/W | Temperature rise per heat flow for a stated sample or assembly | Performance at another area, thickness or pressure | Chỉ sử dụng với hình học và các điều kiện đã nêu |
| Trở kháng nhiệt, K cm2/W | Điện trở chuẩn hóa theo diện tích trong các điều kiện xác định | Nhiệt độ chính xác của mô-đun khi không có dữ liệu hệ thống | So sánh các tiếp giáp ở áp suất và độ dày thực tế |
| Độ nhớt | Khả năng chống chảy trong quá trình thử nghiệm đã nêu | Khả năng nhả khỏi stencil, độ sụt hoặc hiện tượng di chuyển lâu dài của riêng vật liệu | Đối chiếu với nhu cầu in, định lượng và thao tác |
| Nhiệt độ hoạt động | Dải nhiệt độ sử dụng được công bố | Độ ổn định lâu dài theo chế độ chu kỳ nguồn của bạn | Yêu cầu bằng chứng về quá trình lão hóa và xác nhận cụm lắp ráp |
Bảy yếu tố khi lựa chọn mỡ tản nhiệt cho mô-đun công suất
Mỡ tản nhiệt cho mô-đun công suất tối ưu là vật liệu đạt đến nhiệt độ yêu cầu, đồng thời có quy trình sản xuất ổn định và tuổi thọ chấp nhận được. Việc lựa chọn cần kết hợp trở kháng nhiệt tại bề mặt tiếp xúc, độ dày lớp keo có thể đạt được, tính lưu biến, độ ổn định nhiệt độ, khả năng chống di chuyển, tính tương thích và kiểm soát nguồn cung. Một chỉ số nổi bật không thể thay thế sự cân bằng này.
1. Trở kháng nhiệt ở cấp độ cụm lắp ráp
Yêu cầu dữ liệu về trở kháng nhiệt hoặc điện trở nhiệt được đo ở độ dày, áp suất và nhiệt độ cụ thể. Đồ gá thử nghiệm và độ hoàn thiện bề mặt đều ảnh hưởng đến kết quả, vì vậy hãy so sánh các điều kiện tương đương. Nếu các nhà cung cấp sử dụng các phương pháp khác nhau, thứ hạng có thể phản ánh sự khác biệt của phương pháp cũng nhiều như sự khác biệt giữa các hợp chất.
A practical screening test uses representative metal surfaces and several bond lines. The final approval test uses the actual power module and cooler. Record coolant or heat-sink temperature, module case temperature and a repeatable electrical temperature indicator where available.
2. Achievable bond line thickness
Grease performs best when it is thin enough to limit bulk resistance yet thick enough to fill the real surface variation. The achievable bond line depends on:
- Module and cooling-surface flatness.
- Surface roughness and waviness.
- Mounting pressure and screw locations.
- Grease viscosity, yield stress and filler particle size.
- Stencil pattern, deposited volume and squeeze flow.
Các effect of bond line thickness on thermal performance is often larger than buyers expect. Do not choose a nominal coating thickness before studying the mounted joint.
3. Viscosity, thixotropy and stencil printability
Viscosity is only a snapshot of flow resistance. Thixotropy describes how a material changes under shear and then rebuilds after the force is removed. A printable grease should fill the stencil openings, release cleanly, keep its pattern before mounting and spread under clamping without running everywhere.
For automated dispensing, check pressure stability, bead continuity, nozzle size, filler settling and startup after idle time. For stencil printing, check squeegee speed, angle, stencil thickness, aperture geometry and release. A material can have excellent thermal data and still be a headache on the line. That happens more than anyone likes to admit.
4. Operating and peak temperature range
Power modules experience steady heat, short overloads and repeated power cycles. A broad datasheet temperature range does not prove stable viscosity or interface resistance over years of cycling.
Define the real profile:
- Normal case and cooler temperature.
- Maximum continuous temperature.
- Short-duration peak temperature.
- Startup and shutdown frequency.
- Temperature swing and dwell time.
- Expected service life.
Request post-aging data where possible. Then repeat the thermal measurement after cycling, not just before it.
5. Pump-out, dry-out, oil bleed and volatility
These terms describe different problems:
- Hút chất thải is material movement caused by repeated expansion, contraction and pressure changes.
- Làm khô is the loss or redistribution of carrier fluid until the interface becomes filler-rich and less compliant.
- Rò rỉ dầu is visible separation or migration of the liquid phase.
- Volatility is the loss of lower-molecular-weight components, accelerated by heat or low pressure.
Look for stable coverage around hot areas and edges after cycling. A grease that starts with low resistance but migrates away from the active region is not a low-resistance solution in service.
6. Electrical and chemical compatibility
Confirm whether the grease is electrically insulating, slightly conductive or designed only for thermal contact. Also review its interaction with coatings, plastics, labels, seals, connectors and cleaning agents. Silicone oil migration can be unacceptable near optical surfaces, relay contacts, painting or bonding operations. In those cases, evaluate a dầu mỡ nhiệt không chứa silicone or another controlled-chemistry TIM.
7. Manufacturing and supply controls
The supplier should support more than a sample syringe. Production planning needs:
- Packaging suited to printing or dispensing equipment.
- Storage temperature and shelf life.
- Conditioning, mixing or de-airing instructions.
- Batch traceability and certificate data.
- Lot-to-lot rheology and thermal controls.
- Change-notification policy.
- Technical support for stencil and validation trials.
| Engineering question | Property to review | Rủi ro quy trình | Recommended evidence |
| Will the module meet its temperature target? | Thermal impedance at realistic BLT | Datasheet-only selection | Module-to-cooler thermal test |
| Can the layer remain thin and complete? | Rheology, particle size, wetting | Voids or thick areas | Printed mass, thickness and transfer pattern |
| Will it survive cycling? | Pump-out and aging stability | Edge loss or dry zones | Thermal or power cycling plus post-test inspection |
| Can production apply it repeatedly? | Printability or dispensing stability | Lot and operator variation | Capability study using measured deposit mass |
| Is it compatible with the assembly? | Electrical and chemical behavior | Leakage, contamination or coating defects | Compatibility and insulation testing |
How Thick Should Thermal Grease Be on an IGBT or SiC Power Module?
There is no universal grease thickness for every IGBT or SiC power module. Many manufacturer examples sit in the tens to low hundreds of micrometres, but the approved value belongs to a specific module, cooler surface and application pattern. Follow the module mounting document, then verify the compressed interface and thermal result.
For example, Fuji Electric has published guidance around 100 micrometres for selected industrial IGBT modules, including a 100 +/- 30 micrometre example. Mitsubishi literature includes 50-100 micrometres for some module families, while other families use broader ranges. Microchip has documented a minimum value for a specified module and method. These numbers are examples, not a shared industry rule.
Also distinguish deposited thickness from mounted bond line. A stencil creates a patterned deposit with open spaces. During mounting, grease spreads and the peaks collapse. Measuring only the stencil thickness does not reveal the final interface.
A simple grease quantity estimate
For a first estimate:
Mass = coated area x average deposited thickness x density
Suppose a printed pattern has an effective coated area of 90 cm2, an average deposited thickness of 0.010 cm and a grease density of 2.6 g/cm3:
Mass = 90 x 0.010 x 2.6 = 2.34 g
This is a starting process quantity, not an approved specification. Pattern openings, squeeze-out and the mounted bond line change the real result. Weighing the module before and after printing is a useful production check because it measures deposited mass more consistently than a casual visual judgement.
Các Fuji Electric mounting instructions show why grease thickness, heat-sink flatness, roughness and fastening need to be read together.
Heat-Sink Flatness, Roughness and Mounting Pressure Are Part of TIM Selection

The cooling surface can make a suitable grease look bad. Excessive flatness error creates local thick areas or dry contact. Roughness increases the volume needed to fill surface valleys. Uneven fastening changes pressure and may distort the module baseplate. Define these mechanical conditions before locking the grease and stencil.
Flatness and roughness
Flatness describes the overall shape error across the mounting area. Roughness describes the smaller texture left by machining. Both affect contact, but in different ways. A polished surface can still be bowed, and a flat surface can still be too rough.
Inspect the complete module footprint, not a small convenient patch. Module manufacturers often specify acceptable flatness and roughness for their products. Use their limits rather than copying a number from another module family.
Torque and tightening sequence
Mounting screws should usually be tightened in progressive steps and in the sequence specified by the module supplier. Pulling one corner fully down before the others can tilt or bend the module, trap grease and produce an uneven bond line.
Control the tool, torque, screw condition, washer stack and seating surface. For prototypes, mark the sequence and record actual torque. It sounds basic, but this is where quiet variation sneaks in.
Contact pattern inspection
Build sacrificial validation assemblies. Apply the specified pattern, mount the module, then remove it carefully and inspect transfer to both surfaces. Look for uncovered areas, trapped air, edge starvation and excessive squeeze-out.
Combine the visual check with temperature mapping, thermocouples or a module-specific temperature-sensitive electrical parameter. A pretty spread pattern is useful, but the thermal result still decides.
Stencil Printing vs Roller, Spatula and Automated Dispensing
Stencil printing is widely used for power modules because it controls deposited location and volume across a large baseplate. A module-specific pattern allows grease to spread into a thin layer while leaving routes for air to escape. Rollers and spatulas can work in prototypes, but they create more operator variation. Automated dispensing is useful when the pattern and material are designed together.
Why stencil printing appears in OEM guidance
Power modules are larger and mechanically different from desktop processors. A dot or X pattern that looks fine in a hobby video is not a production method for a wide IGBT baseplate.
A stencil can provide:
- Repeatable deposited mass.
- Controlled keep-out around holes and edges.
- Defined islands or tracks for spreading.
- Faster inspection and operator training.
- A measurable relationship between aperture, stencil thickness and deposit.
của Infineon application note on screen-printing templates illustrates the module-specific nature of stencil geometry and process control.
When another method may be acceptable
A roller or controlled spatula can be practical for engineering trials, service work or low-volume builds when the module maker permits it. Dispensing may suit an automated line if the beads merge into full coverage without trapping air. Pre-applied TIM can remove an in-house printing step entirely.
Whichever method is used, define the deposited mass, position, inspection criteria and mounted result. “Apply a thin layer” is an instruction, but not yet a process.
Practical production sequence
- Inspect the module base and cooling surface for damage or contamination.
- Clean both surfaces using approved materials and allow them to dry.
- Condition the grease according to its storage and handling instructions.
- Align the module-specific stencil or dispensing fixture.
- Print or dispense the controlled pattern.
- Inspect position, completeness and deposited mass.
- Mount the module using the specified screw sequence and torque steps.
- Verify transfer pattern and thermal performance on validation units.
| Phương pháp ứng dụng | Volume control | Tốc độ sản xuất | Common risk | Phù hợp nhất |
| Module-specific stencil | High after setup | Cao | Poor release or wrong pattern | Sản xuất lặp lại |
| Việc phân phối tự động | High with calibrated equipment | Trung bình đến cao | Bead gaps, air entrapment, filler settling | Flexible automated lines |
| Roller | Trung bình | Trung bình | Operator-dependent thickness | Approved low-volume assembly |
| Spatula or manual spread | Thấp đến trung bình | Thấp | Uneven coverage and contamination | Prototype or service work |
| Pre-applied TIM | Very high at supplier | High in final assembly | Storage or handling damage | Clean high-volume assembly |
For general handling background, see Haktak’s guide to applying thermal grease.
Common Thermal Grease Failure Modes in Power Electronics
Most thermal grease failures are interface failures, not dramatic material breakdowns. The usual signs are rising or inconsistent temperatures, dry-looking regions, edge accumulation, squeeze-out or contamination. The root cause may be the quantity, stencil, surface, mounting process, aging behavior or cooling hardware. Diagnose the evidence before blaming the jar.
Too much grease
An overly thick layer adds thermal resistance. It may also squeeze beyond the baseplate, contaminate nearby surfaces or interfere with service. More grease does not mean more cooling. The compound is there to replace air, not to become a thick heat-spreading slab.
Too little grease or incomplete wetting
Insufficient quantity can leave air pockets, especially over a bowed baseplate or rough cooler. Local dry areas create hot spots even when the average module temperature looks acceptable. Poor stencil release or an interrupted dispensing bead can produce the same symptom.
Pump-out and edge accumulation
During every heat-up and cool-down cycle, the module and cooler expand by different amounts. Their small relative movement can push a low-stability grease away from active regions. After many cycles, material may gather near edges while the centre becomes thin or dry.
Dry-out, oil separation and viscosity drift
Heat can redistribute or remove carrier fluid. The remaining filler-rich layer becomes less able to wet changing surfaces. Oil bleed may also migrate outside the interface. Check mass, appearance and thermal resistance before and after aging.
Poor surface or mounting control
Variation in flatness, roughness, cleaning, screw torque and stencil alignment often looks like material variation. A good root-cause study compares these records with thermal data by serial number.
| Observed symptom | Nguyên nhân có khả năng cao | Evidence to check | Corrective action |
| High temperature from first build | Thick bond line, voids or poor cooler | Deposit mass, transfer pattern, flatness | Correct surface or pattern, then retest |
| Large unit-to-unit variation | Manual application or torque variation | Weight, stencil position, torque records | Tighten process controls and train operators |
| Nhiệt độ tăng sau các chu kỳ | Pump-out, dry-out or joint movement | Post-cycle coverage and thermal resistance | Screen a more stable grease or revise mechanics |
| Grease around module edges | Excess volume or squeeze flow | Printed mass and edge pattern | Reduce or redistribute the deposit |
| Coating or contact contamination | Oil bleed or incompatible chemistry | Residue analysis and compatibility test | Use controlled-bleed or silicone-free material |
Thermal Grease vs Phase Change Material, Thermal Pad and Graphite
Thermal grease is usually strongest at thin, clamped interfaces that need excellent wetting. It is not automatically best for every module. Phase-change materials can simplify handling, pads can bridge larger gaps or provide engineered insulation, and graphite can spread heat laterally. Compare the actual geometry, electrical needs, production flow and life profile.
| Loại TIM | Best interface | Typical bond line | Assembly advantage | Lưu ý chính |
| Keo tản nhiệt | Flat, tightly clamped module-to-cooler joint | Rất mỏng | Excellent wetting and reworkability | Application variation, pump-out and bleed |
| Phase-change material | Thin clamped joint with clean preform or coating | Thin | Controlled placement and low mess | Must reach activation conditions and wet properly |
| Miếng tản nhiệt | Larger or tolerance-varying gap | Medium to thick | Clean placement, compliance and insulation options | Higher bulk resistance and compression stress |
| Tấm than chì | Lateral heat spreading or selected thin joints | Rất mỏng | Strong in-plane spreading | Electrical conductivity and limited conformity |
A vật liệu giao diện nhiệt chuyển pha may be attractive when a clean pre-applied process and stronger resistance to grease migration matter. Validate activation temperature, pressure and surface contact.
Pads are useful when there is a measurable gap or component height variation. They are not direct replacements for a thin grease joint without redesign. Graphite is highly anisotropic: excellent lateral conductivity does not automatically mean low through-plane interface resistance.
Application Examples Across Power Electronics
Power module grease appears in traction inverters, industrial drives, renewable-energy converters, UPS systems and other high-current equipment. The selection logic is similar, but the dominant stress changes. Automotive systems emphasize severe cycling and contamination control. Industrial systems may prioritize long service, repair and process repeatability. Renewable equipment adds broad ambient conditions and remote operation.
EV traction inverter and onboard charger
An EV inverter may use SiC or IGBT modules mounted to a liquid cold plate. High power density makes a small interface change visible in junction temperature. Qualification should combine coolant conditions, power cycling, vibration and chemical compatibility. The grease must also fit a controlled automotive assembly process.
Industrial motor drive and servo system
Industrial drives run for long periods and may see dust, vibration and irregular maintenance. Consistent stencil application and stable thermal resistance are often more useful than chasing the highest catalog conductivity. Rework and field replacement procedures should use the same controlled quantity as production.
Solar inverter and energy-storage PCS
Solar and battery conversion systems experience daily temperature cycles and wide ambient swings. Pump-out and dry-out screening deserve attention. Haktak’s guide to thermal paste for inverters discusses this operating context in more detail.
UPS, welding and high-power supplies
These systems may have high transient loads and forced-air or liquid cooling. Verify the peak case temperature, mounting pressure and cooler capacity. A short overload may be acceptable electrically but still create a severe interface temperature swing.
Testing Standards and a Realistic Qualification Plan
No single certificate proves that thermal grease will work beneath a power module. Standard methods provide comparable material data, while the final assembly test proves the interface. A sensible plan moves from datasheet review to controlled material tests, process capability, representative module testing and aging. Re-measure performance after environmental stress.
ASTM D5470 and TIM property measurement
ASTM D5470 is widely referenced for steady-state thermal transmission properties of thermally conductive materials. It can be used to derive thermal impedance and apparent conductivity under controlled conditions. ASTM also makes clear that an idealized method does not reproduce every real interface. Surface finish, pressure, thickness and specimen preparation still matter.
JESD51 thermal measurement concepts
The JEDEC JESD51 family provides semiconductor thermal-characterization concepts and methods. These are useful when planning junction-temperature measurements and thermal networks. They are not a standalone thermal grease certification. Apply the relevant method to the device and test objective.
IEC 60068 and application-specific environmental tests
IEC 60068 methods are commonly used as building blocks for dry heat, damp heat, temperature change, shock and vibration testing. Choose tests that reflect the product environment. Automotive, railway, renewable-energy or customer-specific programs may add their own cycles and acceptance limits.
Tổng quan về Haktak các tiêu chuẩn kiểm tra TIM phổ biến can help teams separate material-property tests from assembly reliability tests.
Recommended qualification ladder
- Review documentation. Check TDS, SDS, compliance, storage, shelf life and traceability.
- Run controlled TIM tests. Compare candidate materials at multiple relevant bond lines and pressures.
- Study the application process. Measure deposited mass, position, repeatability and defects.
- Test the representative assembly. Use the real module, cooler, fasteners and coolant or airflow.
- Apply environmental stress. Run thermal cycling, power cycling, humidity and vibration as required.
- Inspect and re-measure. Compare thermal resistance, coverage, bleed, migration and mechanical condition.
What to Send a Thermal Grease Supplier
A useful recommendation starts with assembly information, not a request for “the highest W/mK paste.” Share the module, cooler, temperature target, geometry, mounting process, production method and reliability profile. With that context, a supplier can narrow the chemistry and rheology, propose samples and help define a realistic validation plan.
Prepare the following brief:
- Power module manufacturer, part number and mounting guide.
- Module construction, baseplate size and active heat area.
- Heat-sink or cold-plate material, coating, flatness and roughness.
- Device loss, coolant or ambient condition and temperature limit.
- Maximum allowable interface resistance.
- Screw pattern, torque sequence and estimated clamping pressure.
- Preferred stencil, printing, dispensing or pre-applied process.
- Continuous, peak and cycling temperature profile.
- Vibration, humidity, chemicals and service-life expectations.
- Electrical insulation and silicone restrictions.
- Prototype quantity, annual volume, packaging and traceability needs.
For applications where a very thin interface is the priority, Haktak can evaluate a mỡ tản nhiệt có điện trở nhiệt thấp against the real bond line and production method.
Need to compare candidates in your own module stack? Request samples or a material recommendation with the module drawing, cooler details and operating profile.
Các câu hỏi thường gặp
What thermal grease is best for an IGBT power module?
The best grease is the one that meets the module temperature target at a thin, repeatable bond line and remains stable after the required cycling. Compare interface thermal impedance, printability, pump-out resistance, temperature stability and compatibility. Follow the IGBT manufacturer’s mounting instructions before selecting thickness or application pattern.
How thick should thermal grease be under a power module?
There is no universal thickness. Manufacturer examples often fall in the tens to low hundreds of micrometres, but each value belongs to a particular module and cooler condition. Use the module mounting guide, control deposited mass and verify the mounted transfer pattern and thermal result.
Is higher thermal conductivity always better for power module grease?
No. Higher W/mK can help, but a thicker layer or poor wetting can cancel the benefit. Thermal impedance at the real bond line and pressure is usually more useful. Long-term stability and production repeatability also matter.
Should thermal grease cover the entire module baseplate?
The finished interface should provide effective coverage across the intended heat-transfer area without harmful voids. That does not always mean printing a solid rectangle. Module-specific stencil patterns may use separate deposits that spread during mounting. Follow the approved pattern for the module.
Is stencil printing better than a roller or spatula?
Stencil printing is generally more repeatable for production because it controls volume and location. A roller or spatula may be accepted for prototypes, repairs or low-volume builds if the module maker permits it and the result is inspected. The method must produce the specified mounted interface.
Can thermal grease pump out during thermal cycling?
Yes. Repeated expansion and contraction can move grease away from active areas, especially when the compound, pressure and surface movement are poorly matched. Use thermal or power cycling, inspect coverage afterward and repeat the thermal measurement.
Is power module thermal grease electrically insulating?
Some products are electrically non-conductive, but this should never be assumed from appearance or from the word “grease.” Check the datasheet and safety architecture. A thin compound layer may not satisfy required dielectric, creepage or clearance protection.
When should I use phase-change material instead of thermal grease?
Consider phase-change material when you want clean placement, controlled quantity and reduced handling variation in a thin clamped joint. Confirm activation temperature, wetting, pressure and reliability. Grease may remain preferable where room-temperature wetting and easy rework are important.
How do I calculate the amount of thermal grease for a module?
Estimate mass from effective coated area, average deposited thickness and material density. Then refine it with the actual stencil pattern and mounted transfer test. In production, weighing parts before and after application is a practical way to monitor deposited quantity.
How should thermal grease be tested before mass production?
Start with material and compliance review, then compare candidates at relevant thickness and pressure. Run a process capability study, measure thermal performance in the real module-to-cooler assembly, apply the required environmental cycling, and finally inspect coverage and re-measure thermal resistance.