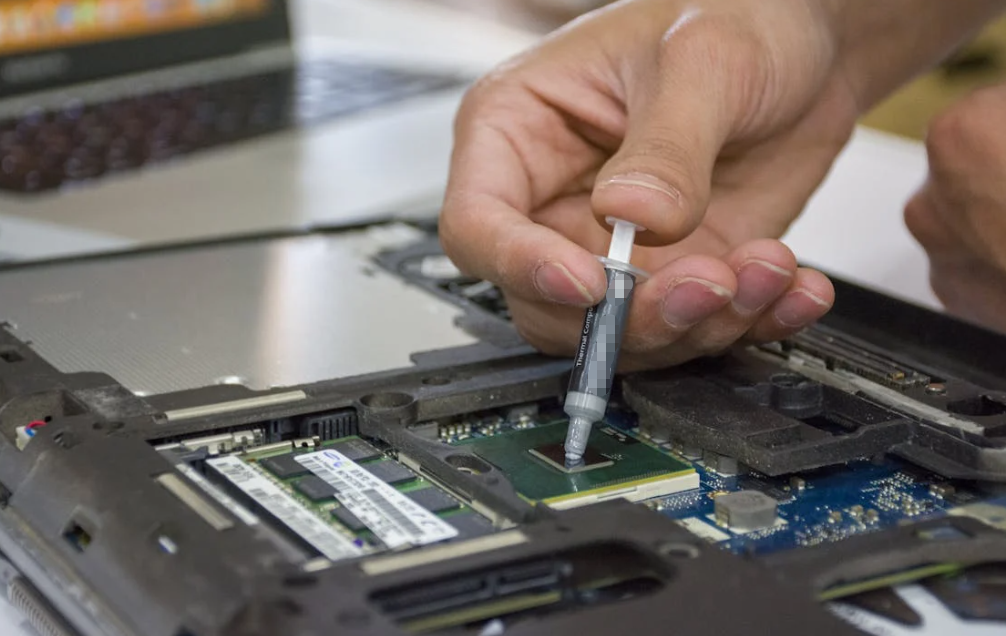
新しいサーマルグリスを塗り、クーラーを取り付け、システムを起動すれば、温度が下がると期待するはずです。しかし、ファンがうるさくなり、温度は上昇します。イライラしますよね。しかし、グリス自体が原因ではないかもしれません。.
サーマルグリスの塗布における失敗のほとんどは、表面の汚れ、不適切な量、不十分な塗布範囲、不均一な取り付け、または不適切な材料の5つのいずれかに起因します。目に見えるパターンはその一部にすぎません。信頼性の高い熱界面には、良好な濡れ性、薄い接合層、安定した圧力、そして再現性のあるプロセスも必要です。.

このガイドでは、何がよく失敗するのか、リスクをどのように判断し、それをどう修正するのかを説明します。CPUやGPUの例を用いることで、その概念を分かりやすく理解できるようになっています。同じ基本原理は、IGBTパワーモジュール、LEDアセンブリ、電源装置、通信ハードウェア、産業用電子機器にも適用されます。.
サーマルグリスが果たすべき役割
サーマルグリスは、クランプされた2つの表面の微細な凹みを埋め、閉じ込められた空気をより熱伝導性の高い材料に置き換えます。薄く連続した界面を形成することを目的としています。構造用接着剤ではなく、通常、大きな機械的隙間を埋めるのに適した材料ではありません。.
金属表面は滑らかに見えるが、拡大してみるとまるで小さな山脈のように振る舞う。プロセッサーの蓋、モジュールのベースプレート、またはLED基板がヒートシンクに触れるとき、最も高い点のみが直接接触する。低い部分には空気が残る。空気は熱の伝導性が低いため、そうした小さな空隙が接触抵抗を増加させる。.
適切な サーマルグリース材料 両方の表面を濡らし、凹凸を埋める。その後、取り付け圧によってグリースが薄い接着層へと押し広げられる。金属は直接接触する部分を通じて熱の多くを伝え続け、グリースは金属同士が接触していない部分を改善する。.
最後の点が重要です。グリスは通常、空気よりも熱をよく伝えますが、アルミニウムや銅よりは劣ります。厚いペーストの層を作ることが目的ではありません。空気を取り除き、接触を維持するのに十分な量が必要ですが、グリスが不必要に長い熱の経路になってしまうほど多くてはなりません。.
同じ預金がなぜ異なる挙動を示すのか
エンドウ豆大の塗布量は1つのデスクトップCPUには機能しても、より大型の長方形のヒートスプレッダの一部を覆い残す可能性がある。あるパワーモジュールで機能するステンシル印刷も、ベースプレートの平坦度が変われば乾燥ゾーンを生み出すかもしれない。結果はインターフェース全体に依存する:
- 接触面積と熱源の位置
- 表面の平面度と粗さ
- グリースの粘度とチクソトロピー
- 取付圧力と締結パターン
- 最終的な結合線の太さ
- 動作温度と向き
- 熱サイクル中の変位
ですから、確かに、塗布方法は重要です。ただ、それだけでは効果を発揮しないのです。.
ミス1:古いグリスや汚れの上からサーマルグリスを塗布すること
新しいグリスで汚れた接触面を修復することはできません。古い化合物、ホコリ、指紋、糸くず、洗浄剤の残留物は、熱の通り道において余分な層となってしまいます。また、これらは新しい材料が表面を均一に濡らすのを妨げ、局所的な抵抗や予測不可能な広がりを引き起こす可能性があります。.

その誘惑は理解できる。古いペーストはまだ柔らかそうに見えるため、もうひと塗り加える程度なら問題ないように思える。しかし実際には、古い層はすでに圧縮され、加熱され、周囲の環境にさらされている。これを新しい材料と混ぜ合わせると、厚さやレオロジー特性が不明な接着層が形成されてしまう。.
再塗布する前に何を取り除くべきですか
- 両方の密着面から古いサーマルグリスを取り除く
- ほこり、糸くず、および浮遊粒子
- 皮脂と指紋
- 切削油または取り扱い油
- 新品のコールドプレートの取り外し可能な保護フィルム
- 洗剤の残留物と湿気
その部品およびクーラーに対して承認されている洗浄方法を使用してください。多くの金属製CPUカバーやコールドプレートの場合、高純度のイソプロピルアルコールと糸くずの出ないワイプが一般的に使用されます。デリケートなプラスチック、コーティング、ラベル、および光学部品については、別の洗浄剤が必要になる場合があるため、まずメーカーの取扱説明書を確認してください。インテルの サーマルグリスの基本的な塗り方のガイドライン 古い材料を取り除き、設置前に表面を乾燥させることも推奨しています。.
簡単な準備ルーティン
- 電源を切り、アセンブリを安全に取り扱える状態にしてください。.
- 表面を傷つけることなく、固まった汚れを取り除きます。.
- 認可されたクリーナーで、両方の嵌合面を拭き取ってください。.
- 表面を完全に乾かしてください。.
- 角度を調整して、明るい光の下でそれらを点検してください。.
- 清掃した接触面に指を触れないようにしてください。.
近くにあるからといって、毛羽立つティッシュペーパーを使用しないでください。薄い接着ラインにかかる1本の繊維は、界面のスケールでは驚くほど大きいです。Haktakのより詳しいガイド(以降未完) サーマルグリスの塗布準備と塗布 実践的な手順をより詳細にカバーしている。.
間違いその2:サーマルグリスの塗りすぎ
過剰なグリスは、特に非導電性のペーストが強力かつ均一な締め付け圧力によって逃げ出せる場合には、それだけで直ちに致命的な問題になるわけではない。それでもなお、余分な材料は接着層を厚くし、汚れを生じさせ、周辺部品を汚染し、不均一な塗布プロセスを隠蔽する原因となり得る。実際の危険性はアセンブリによって異なる。.
オンラインの議論では、この問題は「多すぎるくらいでちょうどいい」対「多すぎるとCPUの絶縁になる」という罵り合いに終始しがちである。どちらの主張も、重要となる条件を無視している。.
2つの平らな面をしっかりと固定し、グリースが外側に流れ出せる状態であれば、余分なグリースの多くは押し出される可能性があります。熱性能は許容範囲内を維持できますが、材料が無駄になり、後片付けが面倒になります。圧力が低い場合や、表面が歪んでいる場合、あるいはペーストの粘度が高い場合、余分なグリースは厚い層となって閉じ込められたままになる可能性があります。これにより抵抗が増加します。.
関係を想像するのは簡単です。熱が薄い塗膜を横切るときは、短い経路をたどります。熱が厚い盛り上がりを横切るときは、周囲の金属よりも熱伝導率の低い物質の中をより遠くまで移動します。ハクタックの説明は 接着剤層の厚さと熱性能 この効果について深く探求する。.
応募数が多すぎる兆候
- インターフェースの大半の周囲からはみ出した多すぎる接着剤
- グリスがソケット、コネクタ、または基板(PCB)の禁止領域に達すること
- 最初の接触の後に滑りやすいクーラーボックス
- 制御された分解後の視覚的に厚い移着層
- 生産ラインにおけるユニット間の大きなばらつき
- 意図したクランプ位置に到達するのが難しい
オーバーフローは電気的リスクも変化させます。多くの一般的なシリコーン系サーマルグリスは電気絶縁性ですが、見た目だけでそうと思い込んではいけません。金属を配合した化合物や液体金属は導電性を持つ場合があります。配線、ピン、露出した部品の近くに漏出させる前に、必ず正確な技術データと安全上の指示を確認してください。.
ミス3:加熱範囲が狭すぎる、またはアクティブ加熱エリアを外している
サーマルグリスが少なすぎると、乾いた部分や空隙が生じます。外周部全体が常に完璧に見た目よく覆われている必要はありませんが、発熱源となるアクティブな領域と本来の接触面は、クーラーに途切れることなく密着している必要があります。高温部分の上のむき出しの部分は、そこから離れた小さな乾いた角よりもはるかに深刻です。.
万能な「エンドウ豆大」という目安は便利なアドバイスであって、普遍的な工学単位ではありません。パッケージの形状はさまざまです。正方形のデスクトップCPU、細長いサーバー用プロセッサ、ベアのGPUダイ、そしてIGBTのベースプレートでは、表面積や熱流束マップは同じではありません。.
補償内容が不十分である可能性を示す手がかり
- 1つの領域、コア、またはデバイスが、同等の領域と比較してはるかに高温になります。
- 負荷をかけるとすぐに温度が上昇する
- 制御された転写インプリントは、熱源の上に乾燥した部分を示しています
- ペーストは大きな長方形インターフェースの中心にのみ到達します
- 同じハードウェアでクーラーを取り付け直すと、冷却結果が変わる
すでに組み立てられたインターフェースの端に少量のグリスを何度も付け足すのはやめてください。塗布状態が本当にはっきりしない場合は、クーラーを安全に取り外し、圧着跡を記録し、両方の表面をきれいに清拭してから、量を管理した塗布でやり直してください。.
高価値のアセンブリでは、実際の部品で作業を行う前に、透明なプレートやテスト用クーポンを使用することでプロセスの開発に役立てることができます。これは開発ツールであり、最終的な熱検証の代わりになるものではありません。.
ミス4:ドット、ライン、X、またはスプレッドのパターンを完全な答えとして扱うこと
あらゆるインターフェースに通用する単一のパターンは存在しません。有用な方法とは、実際の形状、ペースト、および実装システムに対して、再現性のある濡れ性と制御された最終接着ラインを提供する方法です。体積、配置、圧力、および検証は、上面に描かれた形状よりも重要です。.
中央のドットはシンプルで、固定された中程度の表面に対してしばしば効果的です。線状のものは、細長いヒートスプレッダに適している場合があります。X字型はより広い範囲に材料を広げるのに役立ちますが、量がコントロールされていないと交差部分が厚くなりすぎる可能性があります。手動での塗布は目視でカバー範囲を確認できますが、汚れたツール、筋、または繰り返しの擦り取りは新たな問題を引き起こす可能性があります。.
工業用アセンブリでは、ステンシル印刷、スクリーン印刷、または自動ディスペンスがよく使用されます。なぜなら、「だいたいこれくらい」という感覚的な方法は、数千個単位の生産には適さないからです。.
| 方法 | 便利な状況 | よくあるエラー |
| 中黒 | 小さめまたは中サイズのクランプ面 | すべてのパッケージに1つのドットサイズが適合すると仮定する |
| LINEまたはX | 細長い、または大型のヒートスプレッダ | 太く交差するビードを肉盛する |
| 手動スプレッド | 高粘度ペーストまたは視認可能な被覆要件 | 異物混入、スジ(リブ)、および膜厚ムラ |
| ステンシルまたはスクリーンプリント | 再現可能なパワーモジュールの生産 | 不適切な開口部、摩耗した工具、または未検証の印刷厚さ |
| 自動調剤 | 生産量と生産場所の管理 | 校正のずれ、閉じ込められた空気、または不良な吐出経路 |
正しい選択は、インターネットの伝統ではなく、部品を中心に展開されるべきである。ハクタク(Haktak)の比較を参照: サーマルグリスの塗り方 各技術をより詳しく見るために。パワー半導体についても、リテルファューズは公式な サーマルグリース用メタルマスク設計に関するアプリケーションノート.
ミス5:クーラーの不均等な下降または締め付け
クーラーが傾けられたり、横方向に引きずられたり、一箇所だけ完全に締め付けられたりすると、正しい塗布であっても失敗することがあります。不均一な取り付けはグリースを一部の領域から移動させ、局所的な接着層の厚さを変化させ、界面全体に不均一な圧力マップを作り出します。.

グリスを塗布したら、冷却面を垂直にまっすぐ下ろしてください。「ペーストを広げやすくするため」に滑らせないようにします。各固定具を軽く締め始めてから、ハードウェアまたはモジュールメーカーが指定する順序とトルクを使用してください。対角線上のクロスパターンが一般的ですが、ドキュメント化された組み立て手順が優先されます。.
なぜトルクが大きければ大きいほど良いとは限らないのか
クランプ荷重を高めると、ある程度までは接着層(ボンドライン)を薄くし、濡れ性を向上させることができます。しかし、その限界を超えて力を加えすぎると、プリント基板(PCB)のたわみ、はんだ接合部へのストレス、モジュールベースプレートの歪み、またはベアダイの損傷を引き起こす可能性があります。また、有効領域からグリスを過剰に押し出してしまう恐れもあります。.
スプリングワッシャー、ワッシャー、ブラケットは、組み立て体が膨張・収縮する際に圧力を維持するのに役立つため重要です。緩んだ締結部品や底付きした締結部品は、より高価なペーストを選んでも直すことはできません。.
ミス6:クーラーを取り外した後にグリスを再利用する
Once the interface has been separated, the old grease film may not return to the same continuous state. The safest long-term practice is to clean both surfaces and apply fresh material, even when the first application is only a few minutes old.
Lifting a cooler breaks the compressed film. Paste stretches, tears and moves into ridges. Dust may enter before the cooler is replaced. Reseating can trap gaps between those disturbed regions. Sometimes temperatures still look fine, which is why this shortcut survives. But “it booted” is not the same as a controlled process.
For a temporary diagnostic check, an engineer may accept a different level of risk. A final product, customer sample or production assembly needs the documented process. If the cooler comes off, reset the interface.
Do not add fresh paste on top of the disturbed layer. That creates a mixture with uneven thickness and unknown distribution. Clean, inspect and reapply.
Mistake 7: Selecting Thermal Grease by W/mK Alone
A high thermal-conductivity number does not guarantee the lowest device temperature. A grease with strong wetting and a thin stable bond line can outperform a higher-W/mK material that is difficult to spread, too thick in use or unstable during cycling.
Thermal conductivity describes the material. Thermal impedance describes opposition to heat flow through the tested interface under stated conditions. Device temperature also includes contact resistance, spreading resistance, cooler performance and the rest of the heat path.
That is why the label on the syringe is only the start. Review the thermal grease parameters that affect real use, including viscosity, oil bleed, volatility, dielectric behavior and temperature range. Then interpret conductivity alongside thermal impedance and interface conditions.
Properties that should be considered together
- Thermal impedance at a known bond line and pressure
- Apparent or bulk thermal conductivity and test method
- Viscosity, thixotropy and spread behavior
- Operating and storage temperature
- Oil bleed, volatility and filler separation
- Pump-out resistance under cycling
- Electrical conductivity or insulation
- Compatibility with metals, plastics, coatings and seals
A technically modest grease used correctly can beat an impressive datasheet number used badly. Not glamorous, perhaps, but common.
Mistake 8: Ignoring Storage, Separation and Shelf Life
An application can look neat and still fail because the material was expired, separated or stored outside its specified conditions. The syringe, cartridge or jar is part of the process. Grease condition affects dispensing, filler distribution, wetting and long-term stability.

Before use, confirm the product identity, lot number, expiry date and storage history. Look for unusual oil separation, dry crust, lumps or inconsistent color. Some products have an approved conditioning or mixing procedure; others should not be remixed in the field. Follow the technical data sheet.
Never restore a thickened grease by adding solvent or oil. That changes the formulation and invalidates the supplier data. Do not mix two pastes because their colors look similar. Filler chemistry, carrier fluid, additives and electrical behavior may be different.
If old material has hardened at the interface, the detailed explanation of サーマルペーストが乾燥する理由 can help separate storage problems from in-service aging.
Mistake 9: Assuming Good Initial Temperatures Prove Long-Term Reliability
A new grease interface can perform well and then degrade through pump-out, carrier loss, oil bleed or changing contact pressure. Qualification should represent the real thermal cycles, vibration, orientation and service life. A short benchmark proves initial assembly performance, not lifetime stability.
Pump-out happens when repeated expansion and contraction move grease away from part of the active interface. It is especially important around large dies, power modules and assemblies with significant coefficient-of-thermal-expansion mismatch. A vertical orientation may add migration risk for a material with poor slump control.
ハクトクのガイド サーマルグリースの熱サイクルによるポンプアウト explains the mechanism and validation approach.
A realistic power-module example
Imagine an inverter module that passes its end-of-line temperature test. After repeated heat-up and cool-down cycles, one corner begins running hotter. The catalog W/mK value has not changed, but local contact has. Baseplate movement, uneven fastener load and grease displacement may have created a growing dry region.
The useful test is not simply “does it turn on after aging?” Measure the same thermal response before and after the environmental profile. Inspect movement, bleed, cracking and contact where the failure analysis allows it.
Mistake 10: Blaming the Grease Before Checking the Whole Cooling System
High temperature after repasting does not prove the thermal paste is defective. Poor cooler seating, a stopped pump, reversed airflow, the wrong bracket, changed power limits or a misleading sensor can create the same symptom. Troubleshooting should follow the complete heat path.
| 症状 | Possible Grease-Related Cause | Other Cause to Check |
| Immediate high temperature | Poor coverage, forgotten film, uneven seating | Pump disconnected, fan error, wrong bracket |
| One region or core is hotter | Local dry zone or pressure variation | Die layout, sensor behavior, warped surface |
| Temperature rises over weeks | Pump-out, dry-out or migration | Dust buildup, fan wear, coolant problem |
| ユニット間での大きなばらつき | Uncontrolled dispensing or torque | Part tolerance, cooler flatness, test variation |
| Paste reaches nearby components | Excess volume or poor placement | Missing keep-out control or handling error |
Start with what changed. If the cooler was removed, inspect mounting and paste application. If only software changed, check workload and power behavior. If every unit in one batch runs hot, look at material handling, dispensing calibration and assembly settings. Random guesses burn time.
How to Correct a Bad Thermal Grease Application
Do not keep adding paste to an uncertain interface. Record the symptom, rule out obvious cooling-system faults, remove the cooler safely, clean both mating surfaces and rebuild the interface with a controlled material volume and mounting process.
Corrective workflow
- Record a baseline. Note ambient temperature, workload, power, fan or pump state and the sensor being read.
- Check the cooling hardware. Confirm airflow, coolant flow, brackets, springs, screws and electrical connections.
- Remove the cooler safely. Follow the component or module procedure and avoid pulling at an angle.
- Document the transfer pattern. A clear photograph can help reveal dry areas, heavy squeeze-out or pressure imbalance.
- Clean both surfaces. Remove old material and contamination completely.
- Inspect flatness and damage. Look for scratches, bowing, dents and foreign particles.
- Confirm the grease condition. Verify the product, lot, storage and expiry.
- Apply a controlled amount. Use the developed pattern, stencil or dispense program.
- Mount evenly. Follow the approved fastener sequence and torque.
- Repeat the same test. Compare results under the original load and ambient conditions.
If the second application is still poor, stop repasting blindly. Investigate the cooler, mechanical stack, power level and measurement method.
Preventing Thermal Grease Application Errors in Production
Repeatability comes from controlling material condition, dispense volume, location, tooling and clamp load. Operator experience is useful, but a production process that depends entirely on feel will drift between people, shifts and lots.
Manual syringe application may be suitable for prototypes or low volume. As production increases, define what operators can inspect and what equipment must control. A calibrated dispenser can manage shot volume and location. A stencil can create a repeatable printed area. Torque-controlled fastening can reduce pressure variation.
Process controls worth documenting
- Approved material, supplier and lot traceability
- Storage, conditioning and open-time limits
- Dispense mass, volume or printed thickness
- Needle, nozzle, screen or stencil condition
- Placement path and PCB keep-out zones
- Fastener sequence and torque
- Rework and cleanup method
- First-article and periodic thermal checks
- Aging requirements for high-risk products
A compact inspection plan
| 制御 | What It Catches | Possible Record |
| Material and lot check | Wrong or expired grease | Traveler, barcode or batch record |
| Dispense volume or weight | Too much, too little and equipment drift | Shot log or sample weight |
| Visual placement check | Offset deposit, void, overflow and contamination | Approved limit sample or vision result |
| Fastener control | Uneven or insufficient pressure | Torque-tool record |
| Thermal baseline | Combined interface and assembly problems | Temperature rise or thermal-impedance result |
| Post-aging comparison | Pump-out, dry-out and contact loss | Before-and-after thermal data |
The goal is not to inspect quality into the product after assembly. It is to make a bad application difficult to produce in the first place.
What ASTM D5470 Can and Cannot Tell You
ASTM D5470 supports thermal-impedance measurement and apparent-conductivity calculation under defined fixture conditions. It is valuable for comparing thermal interface materials, but it does not certify a finished application volume, mounting process or aged electronic assembly.
The official ASTM D5470 standard page describes a method covering materials from liquid compounds to hard solids. Results depend on specimen thickness, pressure, temperature, contact surfaces and the method used to separate bulk and contact effects.
When reviewing data, ask:
- どのような圧力が加えられたのでしょうか?
- What bond-line thickness was measured?
- At what temperature was the test run?
- Were the contact surfaces comparable?
- Is the reported number conductivity, resistance or impedance?
- Was the material tested before or after aging?
Use a standard to improve measurement consistency, not to avoid assembly testing. Haktak’s overview of 一般的なTIM試験規格 explains where D5470 and related methods fit.
When Thermal Grease Is the Wrong Interface Material
Grease works best between thin, reasonably flat and mechanically clamped surfaces. If the design has a large variable gap, needs clean preformed placement, cannot maintain pressure or requires structural attachment, another thermal interface format may be more reliable.
Consider alternatives when the assembly needs:
- Gap filling across large height tolerance
- A controlled preformed thickness
- Clean placement with no squeeze-out
- Better resistance to migration in a vertical orientation
- Adhesive attachment between parts
- Simplified field service or automation
A thermal pad can cover a designed gap and provide electrical insulation. A liquid gap filler can conform around mixed component heights. A phase-change material offers solid handling before it softens in operation. A thermally conductive adhesive creates a bonded heat path.
For thin, flat and strongly clamped interfaces, 低熱抵抗グリス remains a strong option. The point is to use it where its behavior fits the mechanics, not because paste is familiar.
Information Haktak Needs to Review an Application
A useful thermal-grease recommendation starts with the actual heat source, mating surfaces, expected bond line, clamping method, application process and reliability profile. A close-up photo helps, but it cannot show pressure, power or service conditions by itself.
Send as much of the following as the project allows:
- Component, module or assembly type
- Normal and peak power dissipation
- Heat sink or cold-plate material and finish
- Contact area, flatness, gap and tolerance
- Target component temperature or interface resistance
- Clamp pressure, screw layout and service orientation
- Manual dispense, automation, stencil or screen-print process
- Operating temperature, thermal cycling, vibration and life target
- Electrical insulation, outgassing or silicone restrictions
- Sample quantity and expected production volume
Haktak can use this information to support thermal material selection and application testing before a process moves into production.
結論
The most common thermal grease mistakes are not mysterious: contaminated surfaces, uncontrolled quantity, incomplete coverage, uneven mounting, reused paste and weak verification. What makes them tricky is that several can create the same symptom.
Do not judge the interface by the drawing pattern alone. Clean both surfaces, use a suitable grease, control the amount, mount the cooler evenly and test the complete cooling system under a repeatable load. For production equipment, add traceability, calibrated dispensing, torque control and aging checks.
A good grease application is a little boring. It looks the same from unit to unit, behaves predictably and gives engineers very little to argue about later. That is exactly what you want.
よくあるご質問
What is the most common mistake when applying thermal grease?
Using an uncontrolled amount on an unprepared surface is the broadest recurring mistake. Too much, too little and contamination all change the final interface. Clean both mating surfaces, confirm the correct material, control the deposit and mount the cooler evenly. The pattern matters less than the final wetting, bond line and pressure.
What happens if I apply too much thermal paste?
Excess paste may squeeze out harmlessly under strong, even pressure, but it can also leave a thicker bond line, make the cooler slide and contaminate nearby parts. Electrically conductive compounds create additional risk. If the paste has reached a socket or PCB area, follow the material and hardware cleaning instructions before powering the assembly.
Can too little thermal grease cause overheating?
Yes. Too little material can leave dry contact zones and air-filled voids, especially over the active heat source. That raises local interface resistance and may create hot spots. The correct quantity depends on the contact area, package shape, grease rheology and mounting pressure rather than a universal dot size.
Is it better to spread thermal paste or let mounting pressure spread it?
Either method can work. A center deposit is simple when pressure and geometry spread it reliably. Manual spreading can help with viscous material or a coverage requirement, but the tool and surface must stay clean and the film must remain thin. Production parts often benefit from a developed stencil, screen or automated dispense process.
Do I need to remove old thermal paste before applying new paste?
Yes for a dependable final assembly. Old compound may contain dried regions, contamination and an already-compressed filler structure. Adding new paste on top creates an uneven, unknown bond line. Remove the old material from both surfaces with an approved method, let them dry and then apply fresh grease.
Must I reapply thermal grease after removing the cooler?
Reapplication is the safest long-term practice. Removing the cooler breaks the compressed film and can create ridges, dry zones or trapped voids when it is reseated. Even if the paste is fresh, clean both surfaces and rebuild the interface before final use or qualification.
Can air bubbles in thermal paste cause high temperatures?
Large or poorly located voids can reduce contact and create a hot spot because air conducts heat badly. Still, not every tiny visible bubble causes a measurable problem. Focus on complete wetting over the active region, controlled volume, straight mounting and even pressure rather than trying to eliminate every microscopic void by guesswork.
Can thermal grease damage or short a circuit board?
It depends on the product. Many thermal greases are electrically insulating, while metal-filled compounds and liquid metal may conduct electricity. Even insulating grease can contaminate connectors or make later service difficult. Check the exact datasheet and keep the material inside the approved application area.
Why are temperatures still high after replacing thermal paste?
The cooler may be seated unevenly, a protective film may remain, the fan or pump may not be operating, airflow may be wrong or the test workload may have changed. The paste may also have poor coverage or an excessive bond line. Compare the complete cooling system against a controlled baseline before blaming one material.
How can a manufacturer keep thermal grease application consistent?
Define the approved grease, storage rules, deposit volume, placement area, application equipment, fastener sequence and torque. Use calibrated dispensing or printing where volume justifies it. Record material lots, inspect tooling, establish visual limits and compare thermal performance before and after relevant aging. Repeatability should come from the process, not operator memory.